Skip to content
01632 960863quotes@kestrow.co.ukMonday to Thursday 7:30 to 17:00, Friday 7:30 to 13:00Drawings: STEP · DXF · PDF

Illustrative projects

Case studies

Four projects of the kind a firm like ours takes on, with the figures that matter to a buyer. They're illustrative: Kestrow is a demonstration, so there are no clients to name. A real site's case studies would carry real ones, with permission.

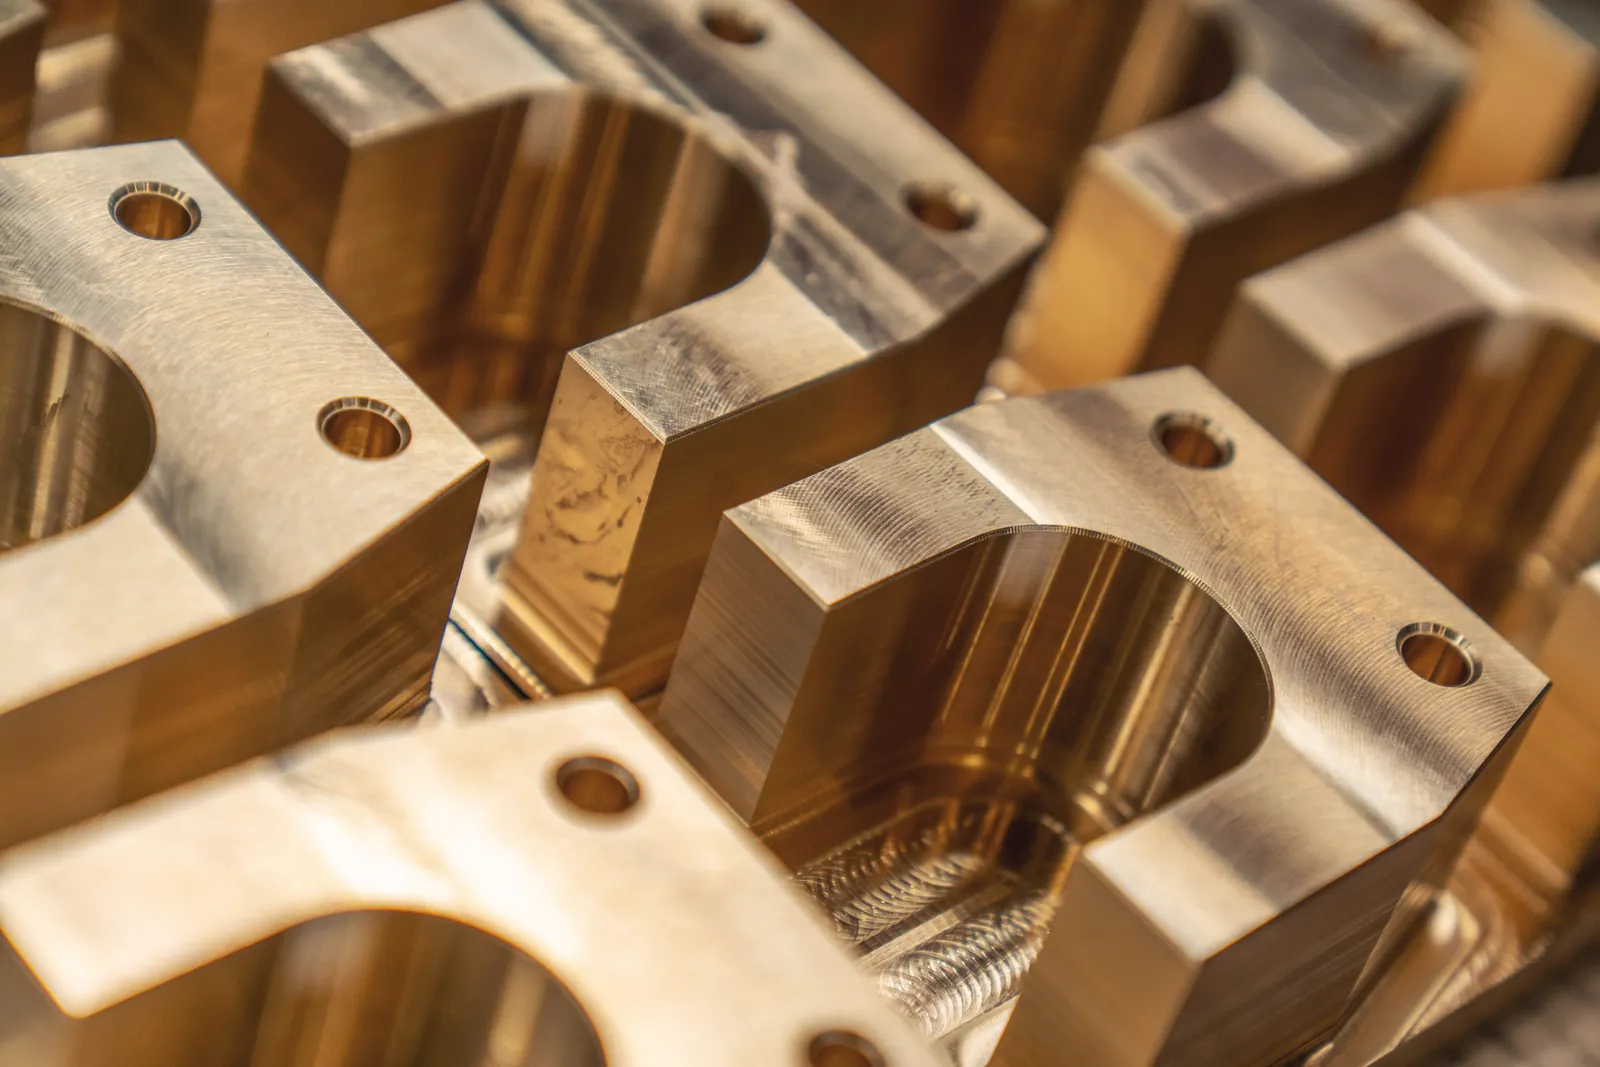
Rows of machined brass brackets with drilled holes, close up
Fig. 1.1Machined brass, after deburr
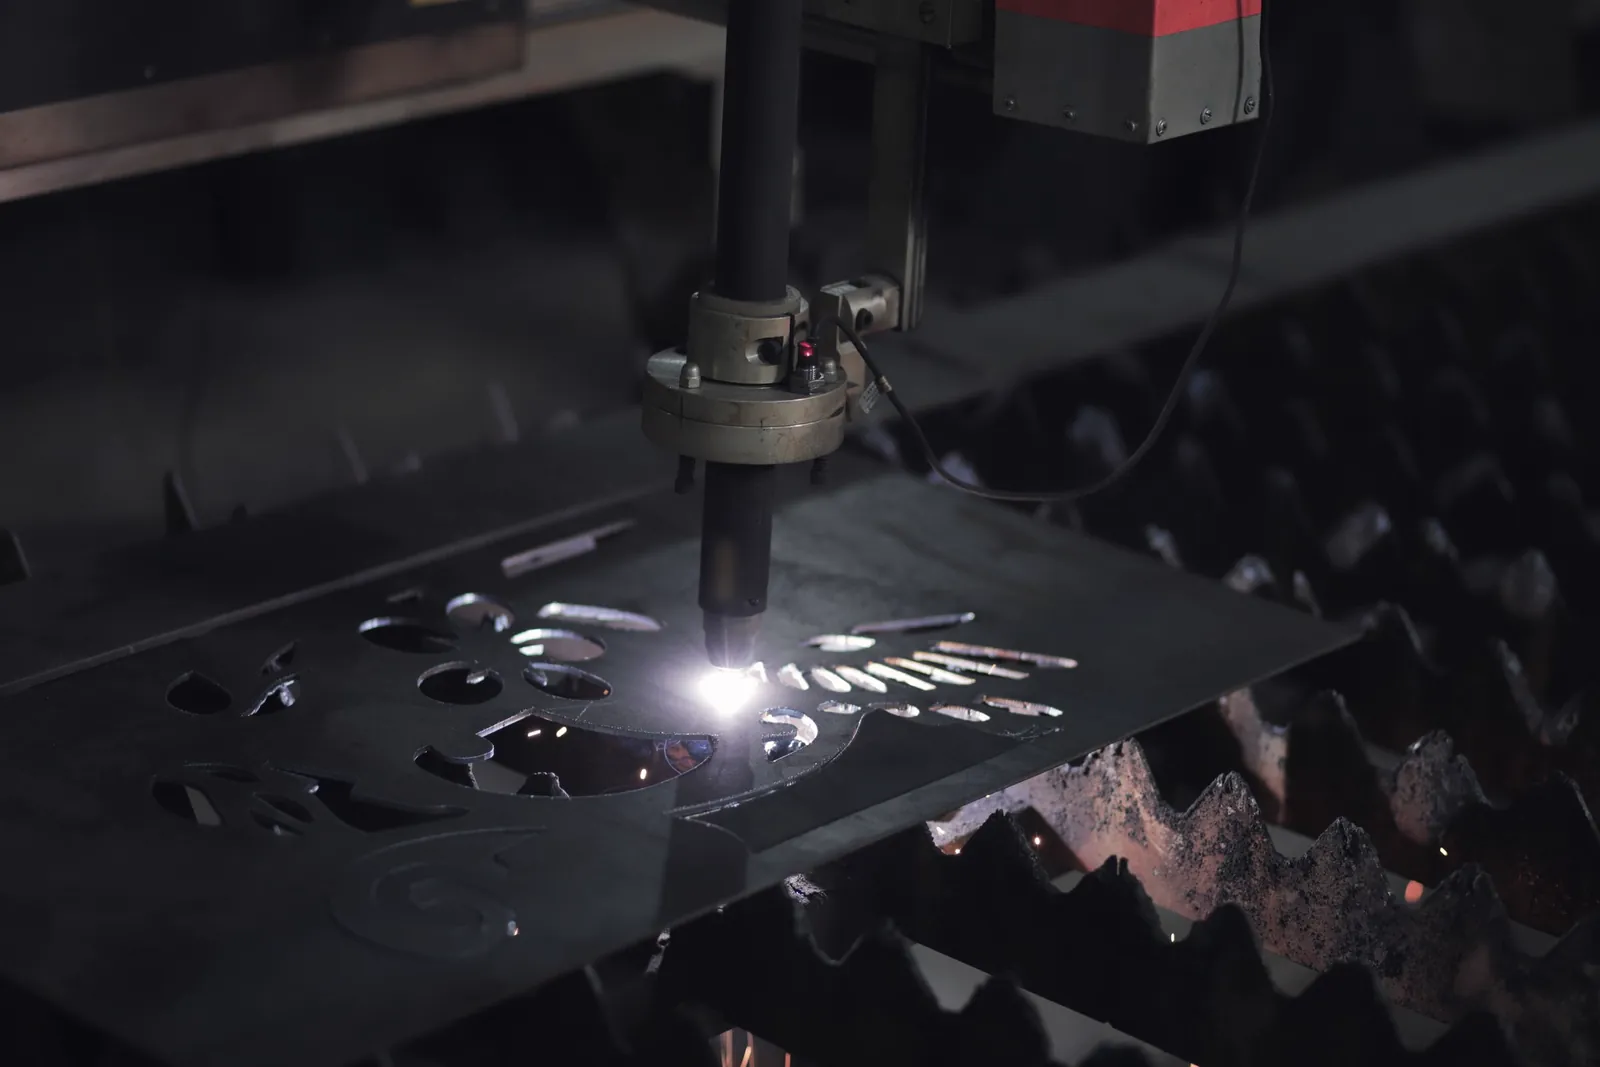
A CNC plasma torch cutting shapes from a steel plate on a slatted cutting bed

Project 01 · Fluid power

Illustrative project

A manifold block: four set-ups to one.

A hydraulics maker was buying a cross-drilled aluminium manifold that took four set-ups on a 3-axis machine, with the gallery intersections deburred by hand.

The brief
Cut the lead time and the scrap on a 24-port manifold, called off in batches of 200.
What we did
Moved it to the 5-axis trunnion machine in one set-up, with a proven deburring tool path for the internal intersections, then hard anodised through a partner and pressure tested before shipping.
The outcome
Lead time from six weeks to three, positional tolerances held at 0.02 mm, and no hand deburring left in the process.
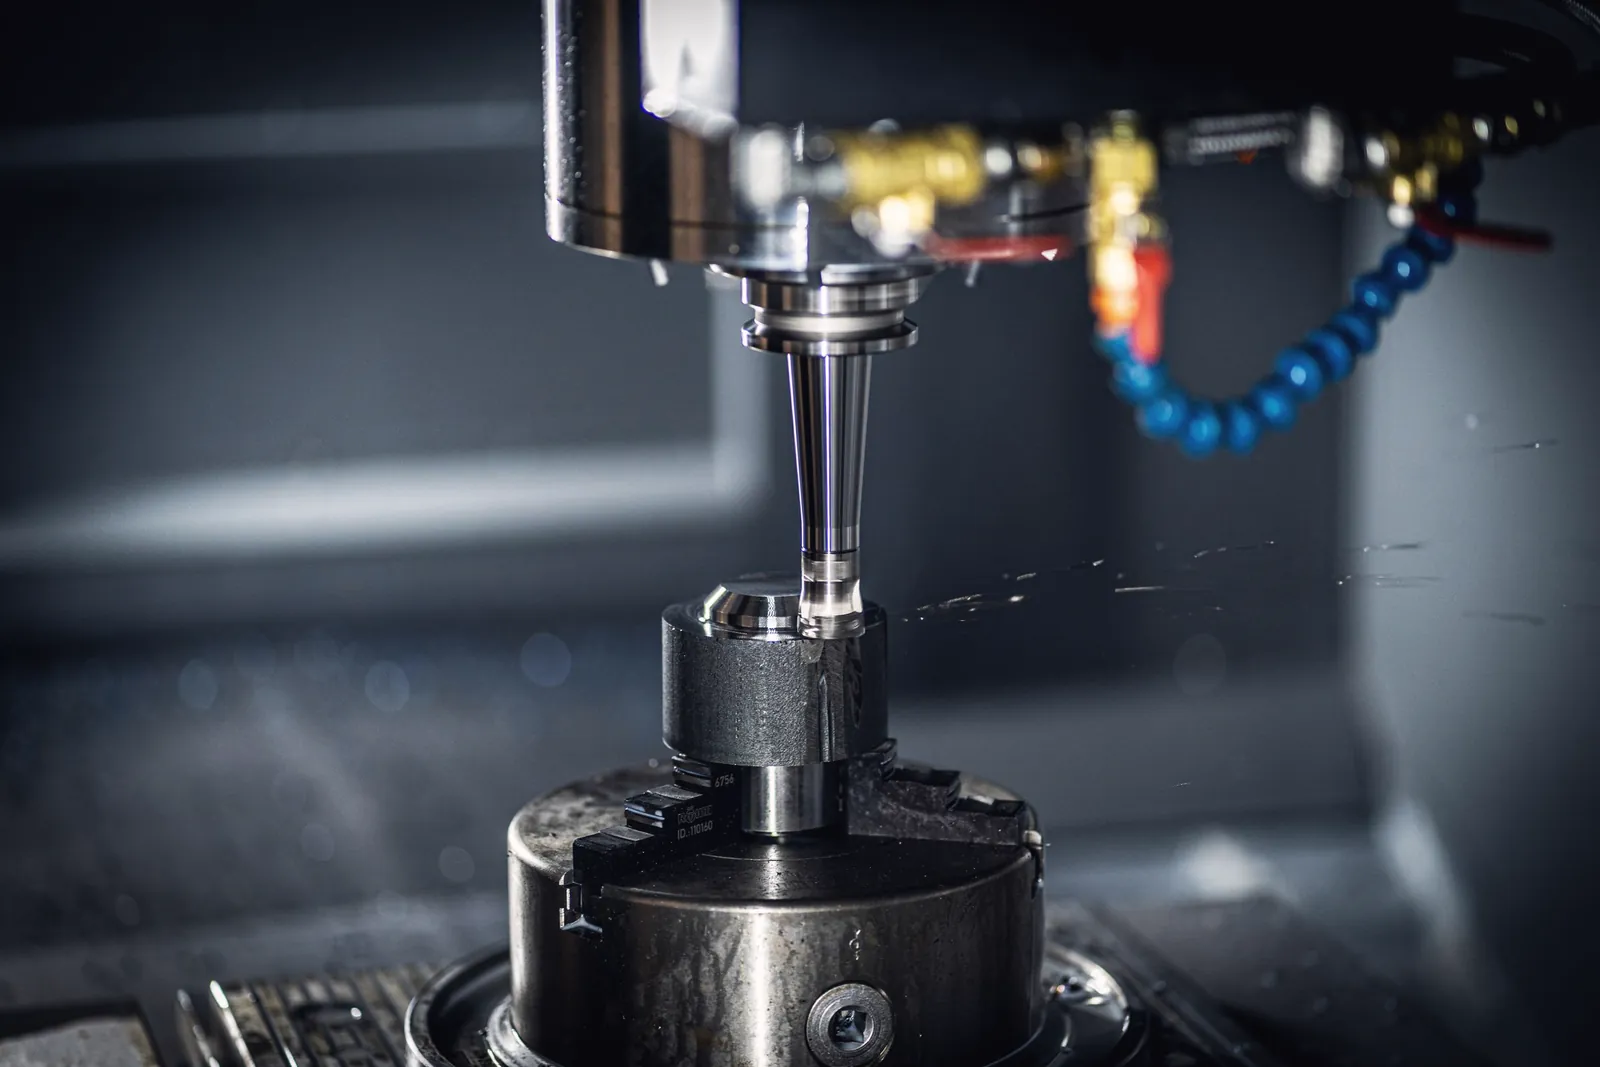
A milling cutter in the spindle of a CNC machining centre, above a part held in a three-jaw chuck, coolant line beside it
Fig. 2.1Finishing pass, vertical machining centre
A drill plunging into an aluminium plate as coolant splashes around it
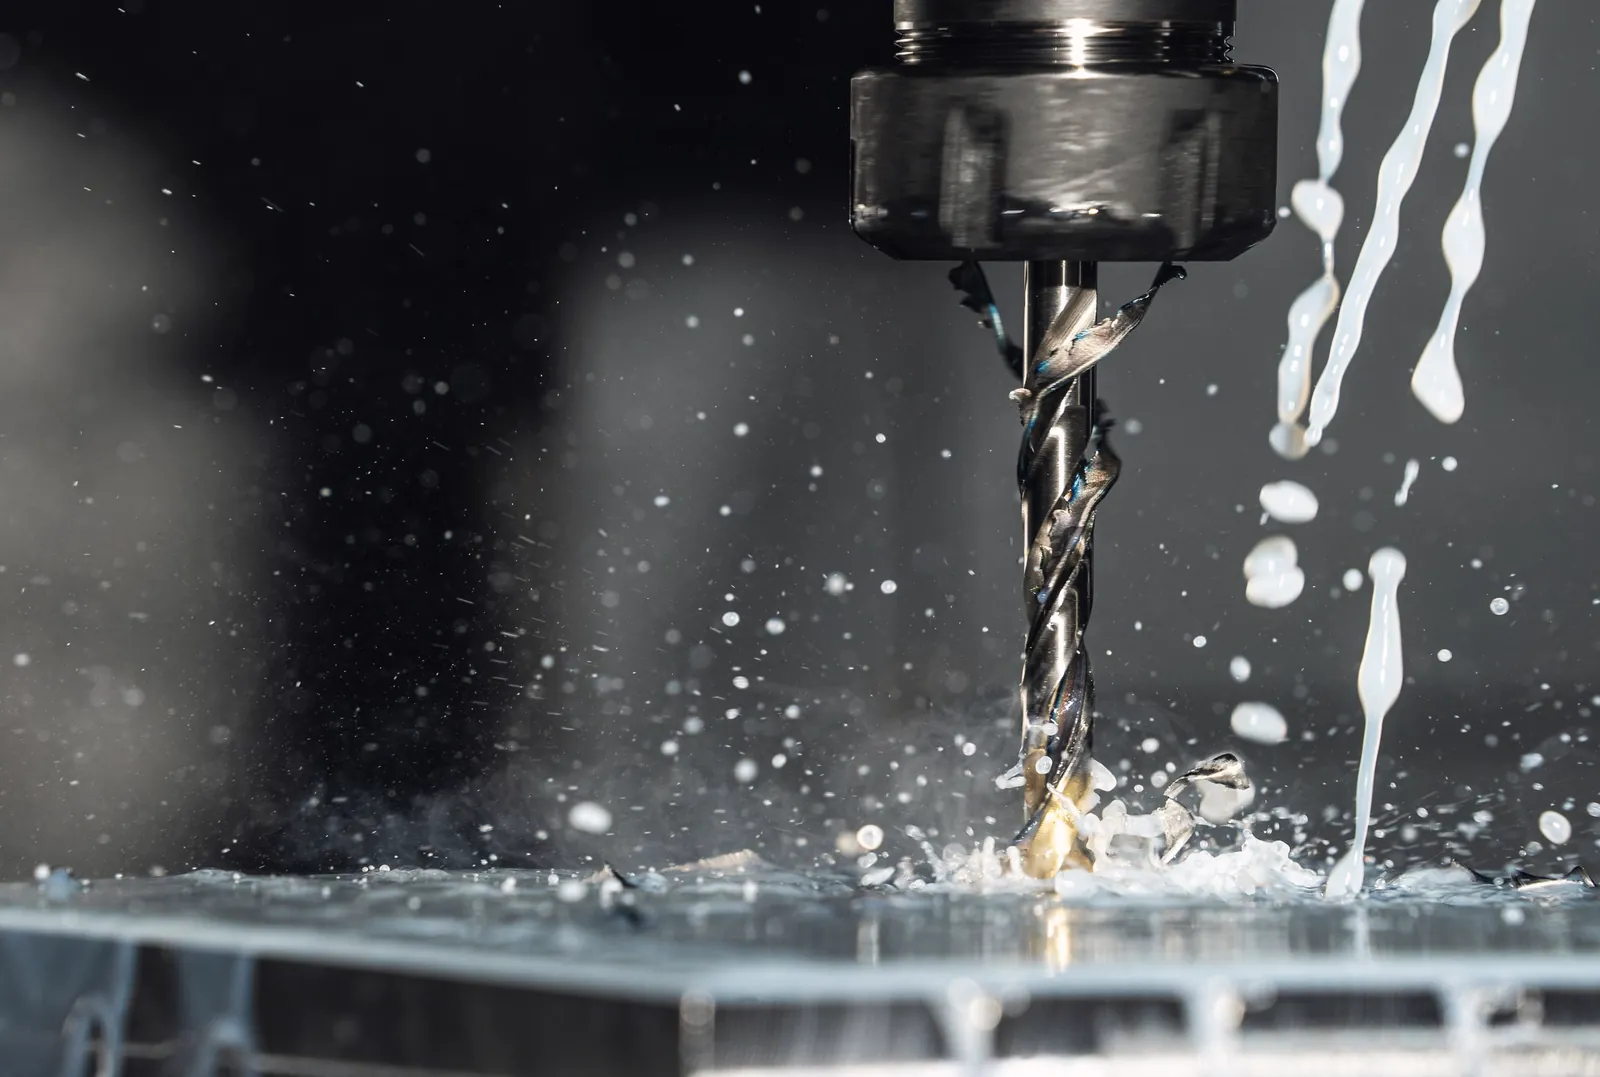
Fig. 2.2Drilling through coolant
MaterialProcessBatchKey tolerance
6082-T6 aluminium5-axis milling, hard anodise, pressure test200, on call-off0.02 mm true position

Project 02 · Medical devices

Illustrative project

Stainless pins, ten thousand a month.

A device maker needed a second source for a small 316L pin with a cross hole and a polished end, without restarting its validation.

The brief
Match the existing supplier's part exactly, with lot traceability from bar to bag and a full first-article report.
What we did
Ran it complete on a sliding head with back working, so the cross hole and end polish need no second operation, then passivated through a partner and bagged to the customer's lot numbers.
The outcome
First articles accepted on the first submission, and 10,000 a month delivered against a rolling schedule.
A heap of turned stainless steel rings, catching the light
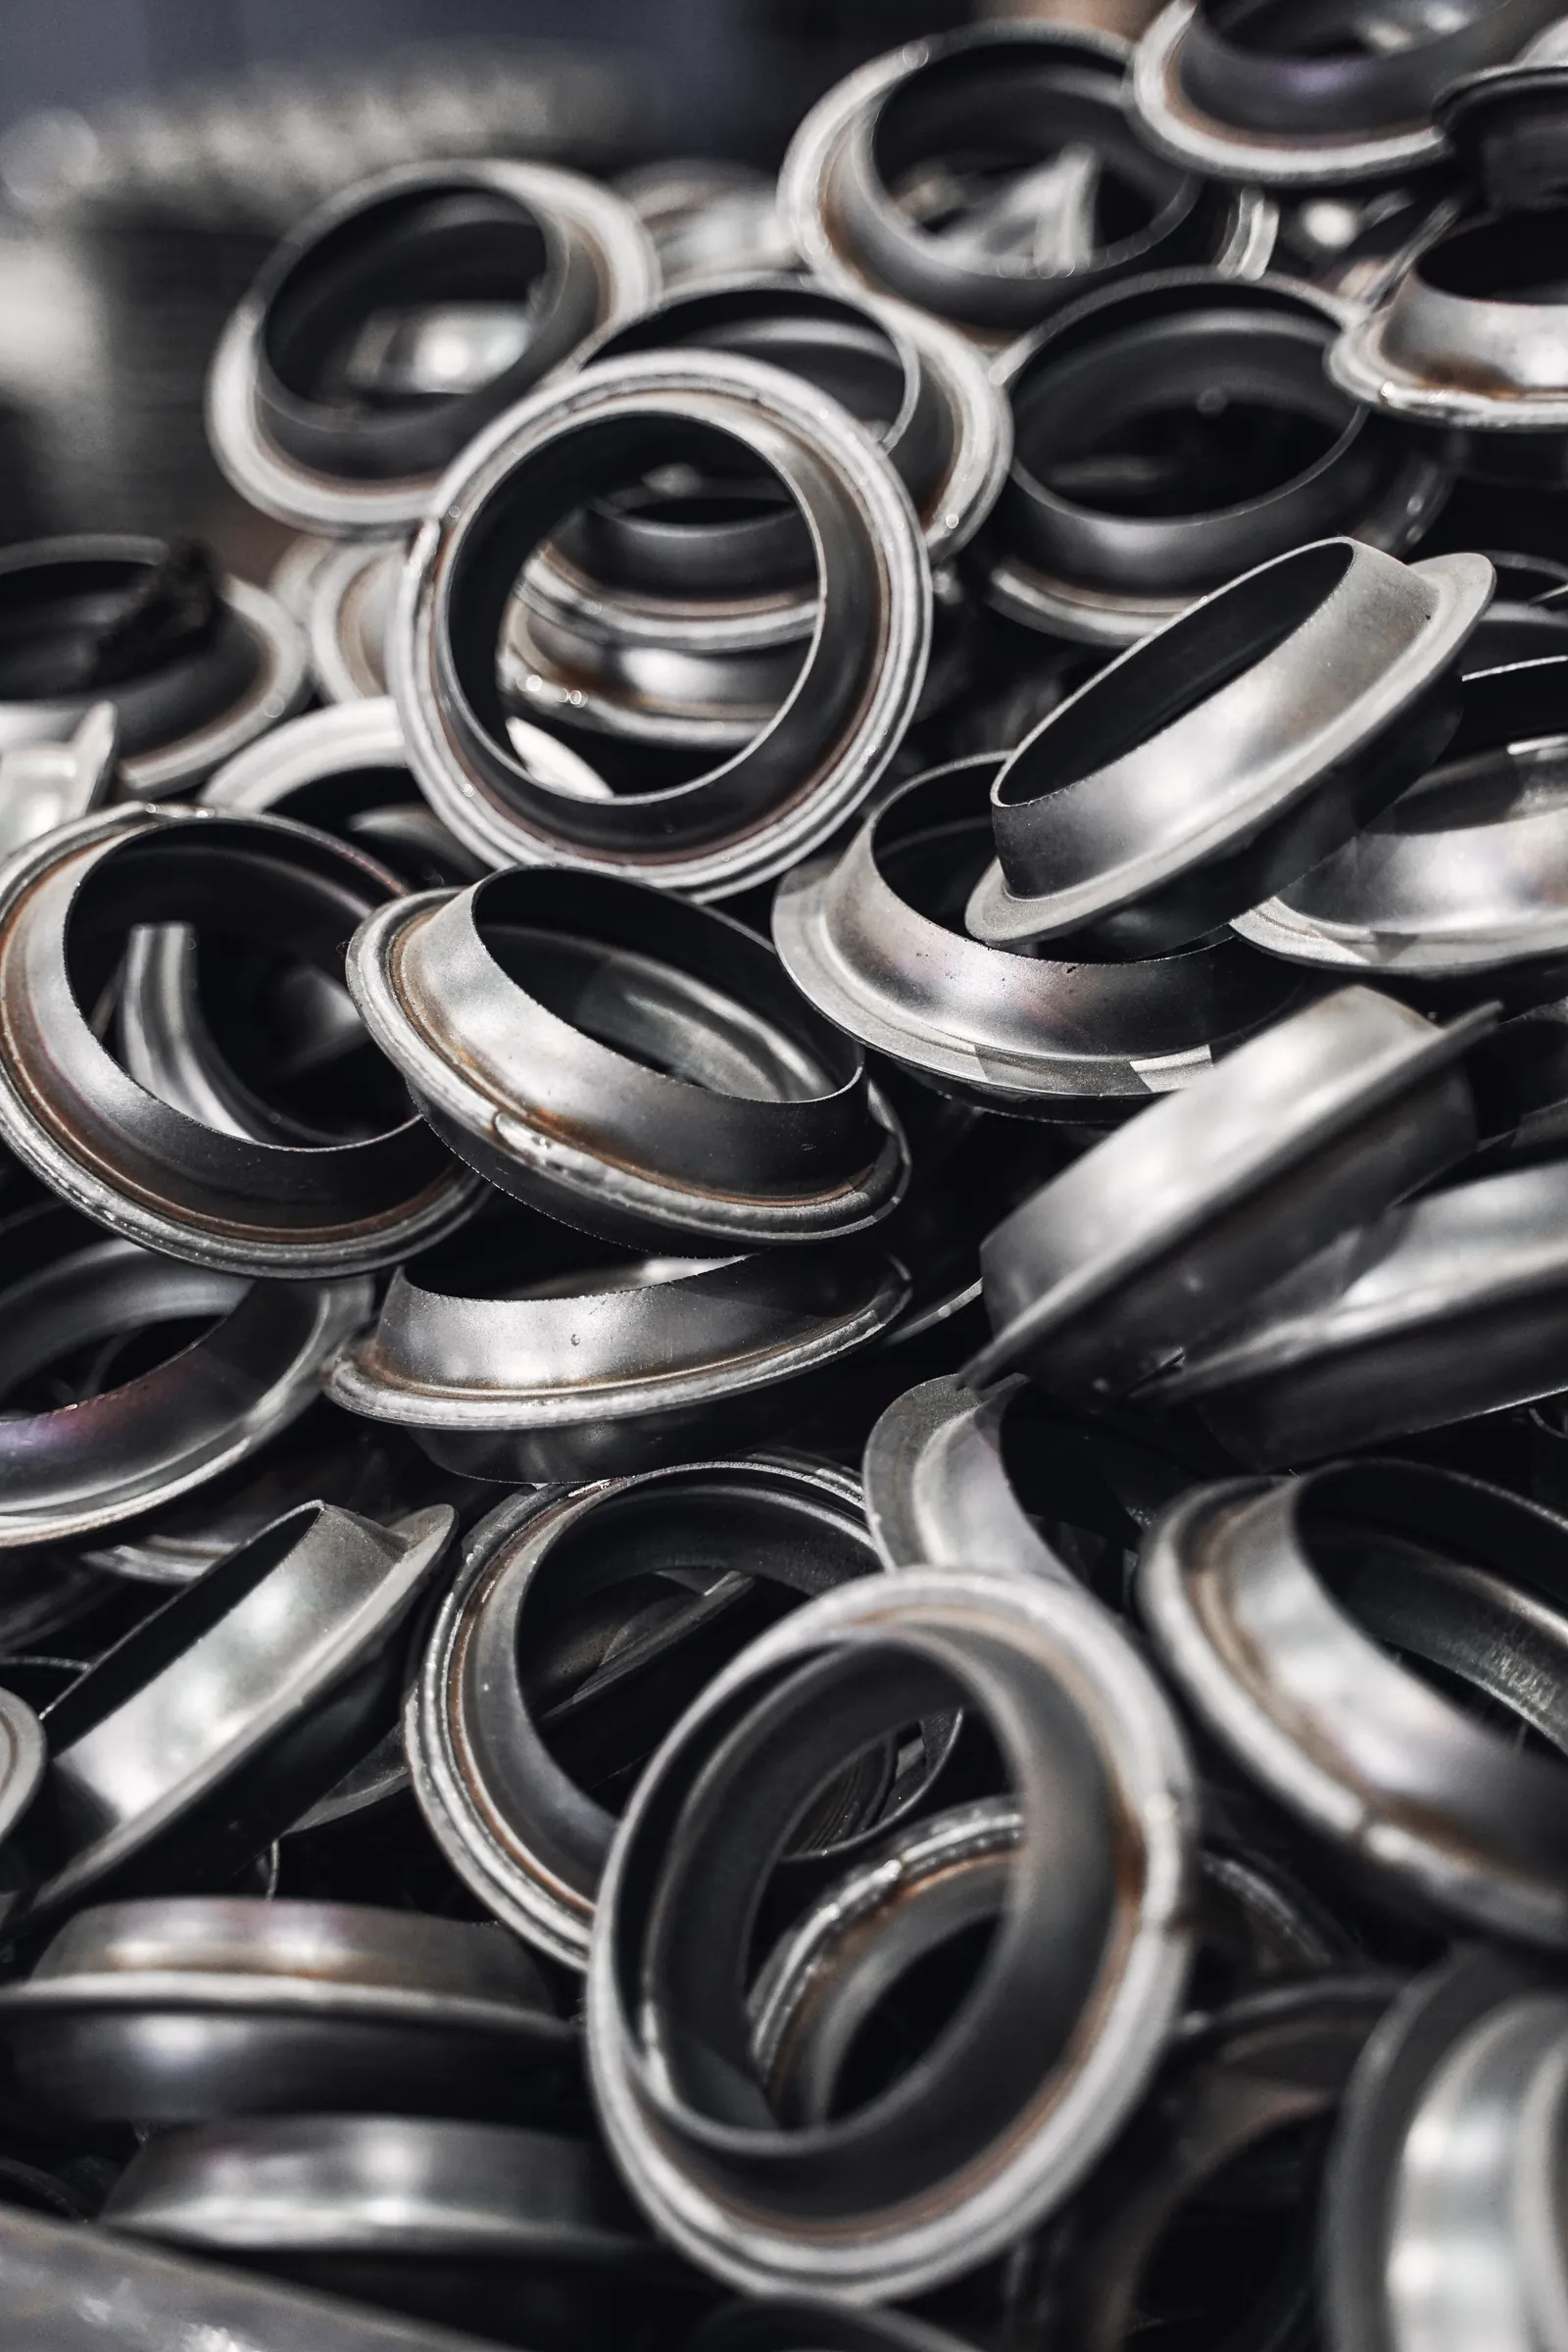
Fig. 3.1Turned rings, one batch
A single machined part with a straight-knurled surface on a dark background
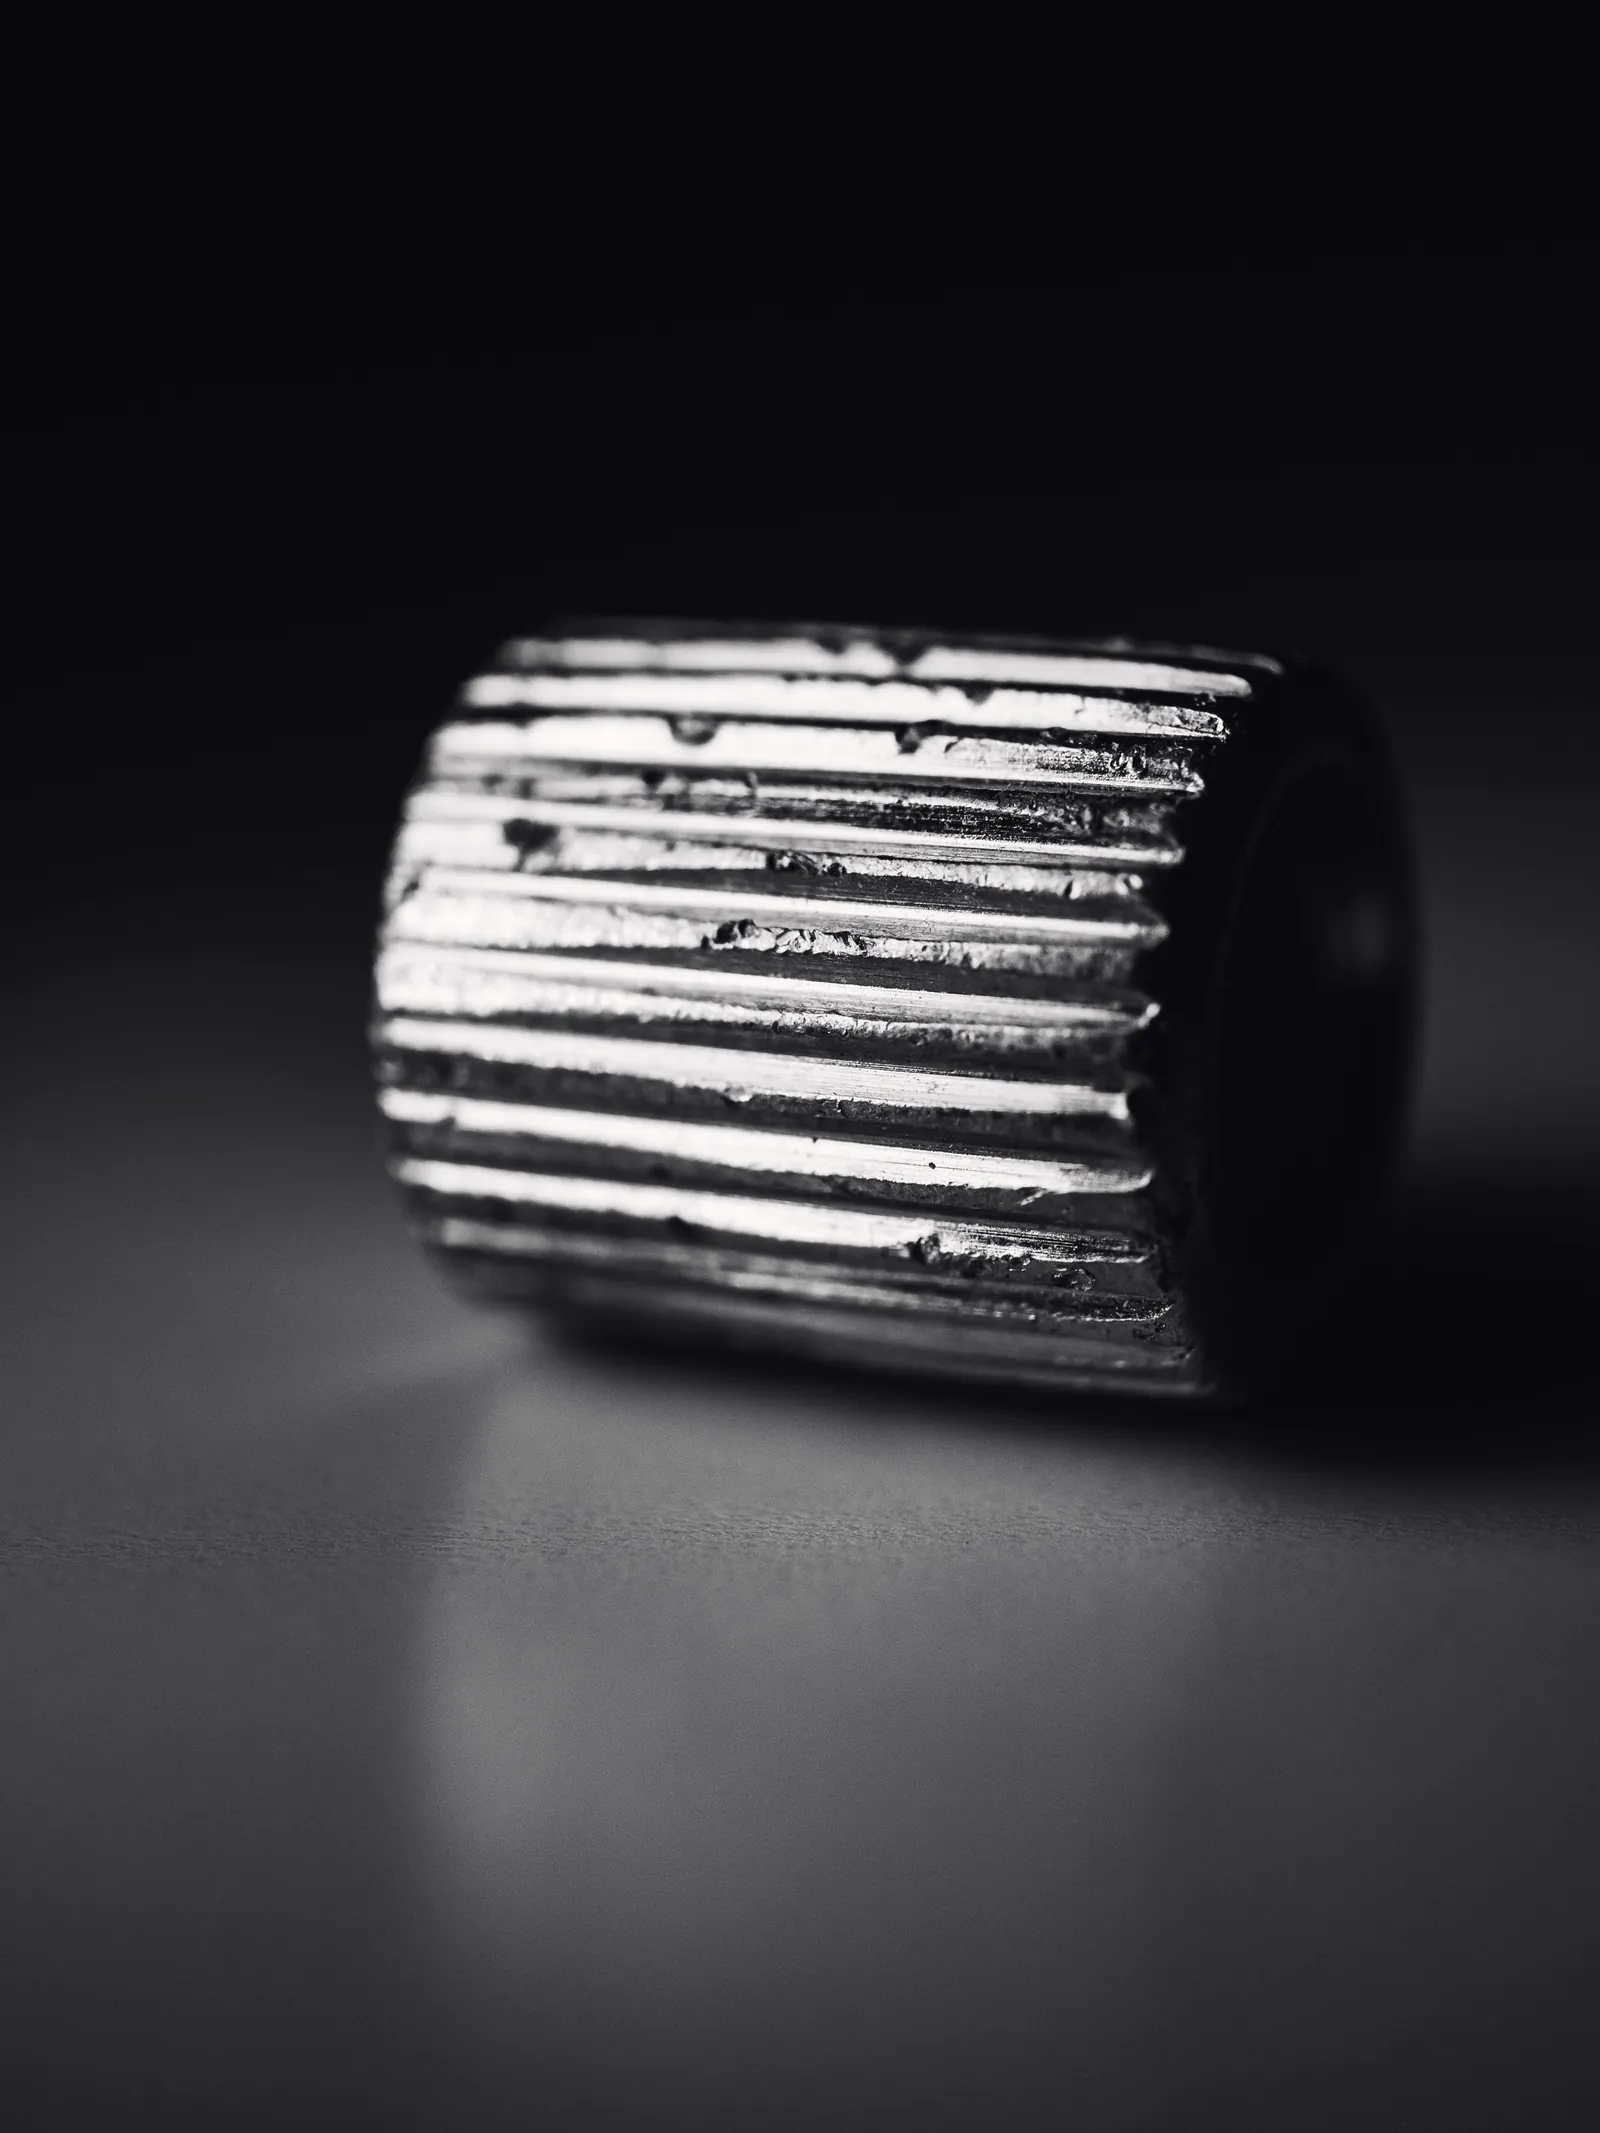
Fig. 3.2Knurled sleeve
MaterialProcessBatchKey tolerance
316L stainlessSliding-head turning, passivation10,000 a monthØ 4 mm, ±0.005 mm

Project 03 · Packaging machinery

Illustrative project

A machine frame, welded then machined.

A packaging machine builder was buying its frames from a fabricator, then sending them to a machine shop for the bearing faces, then to a coater.

The brief
One supplier for the finished frame, with the datum faces machined true after welding.
What we did
Laser cut and folded the panels, welded them in our own fixture, stress relieved through a partner, machined the faces on the bridge mill and sent them to be powder coated.
The outcome
Three suppliers became one, two deliveries and a week left the lead time, and the frames arrive ready to build on.
Gloved hands welding a steel frame, sparks and smoke rising from the joint
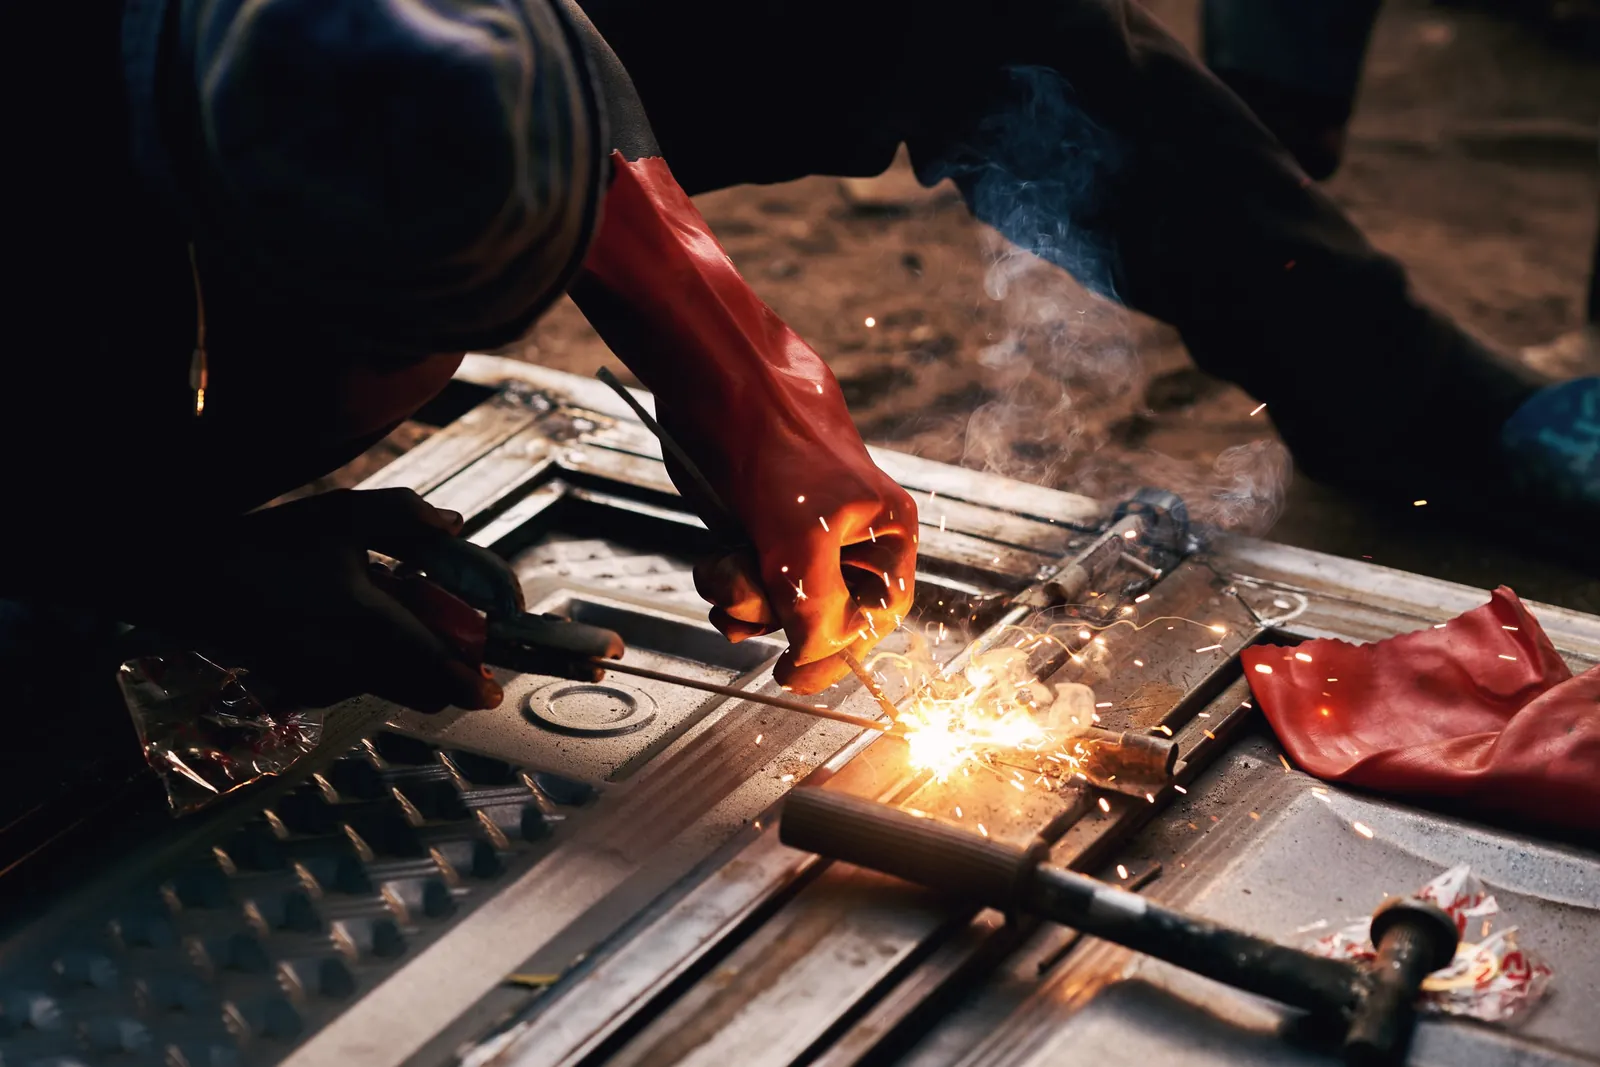
Fig. 4.1Tacking a frame
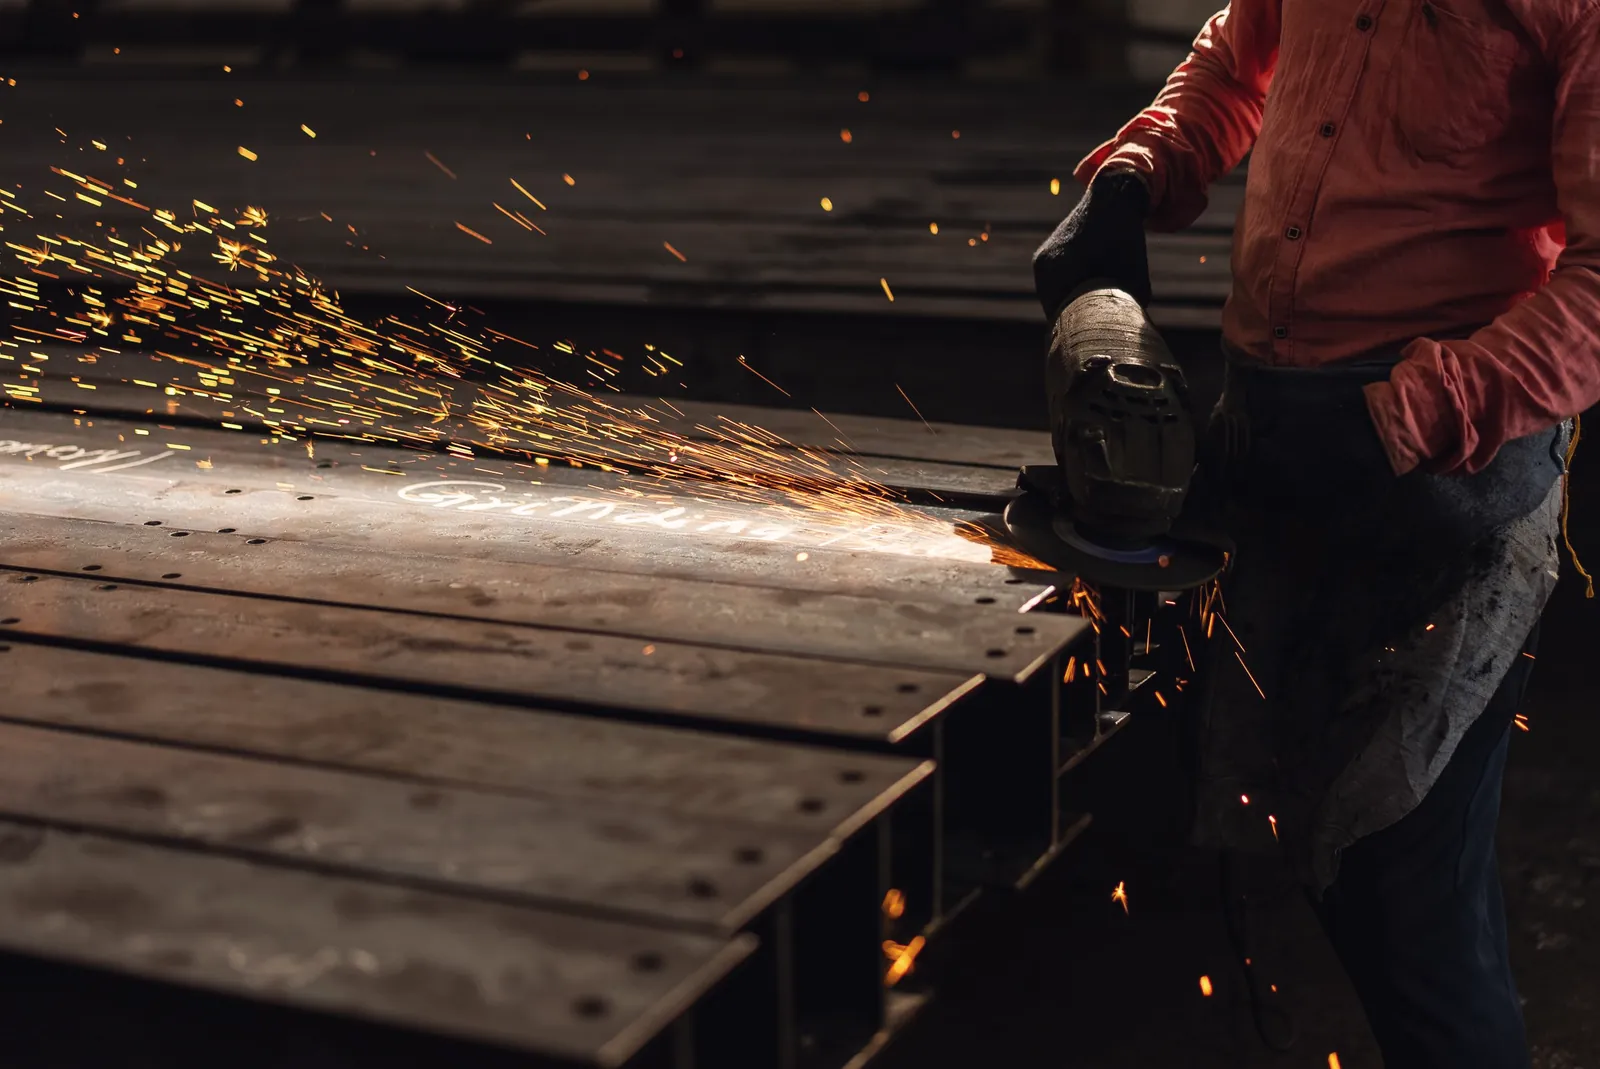
A gloved fabricator grinding a weld along a steel beam, sparks spraying across the workshop
Fig. 4.2Dressing welds on a beam
MaterialProcessBatchKey tolerance
S275 steel plate and boxLaser, fold, MIG weld, machine, coat12 a quarter0.05 mm flatness on datum pads

Project 04 · Electric drives

Illustrative project

A gearbox housing, prototype to production.

An electric drive start-up needed five prototype housings in a fortnight, and a plan to make thousands if the design worked.

The brief
Prototypes fast, machined from billet, and a route to volume without a second qualification.
What we did
Machined the prototypes from solid on 5-axis, suggested two design changes that saved a set-up, and kept the same fixtures and programmes ready for production.
The outcome
Prototypes in nine working days; production started on the same programmes, the first batch released on its first-article report.
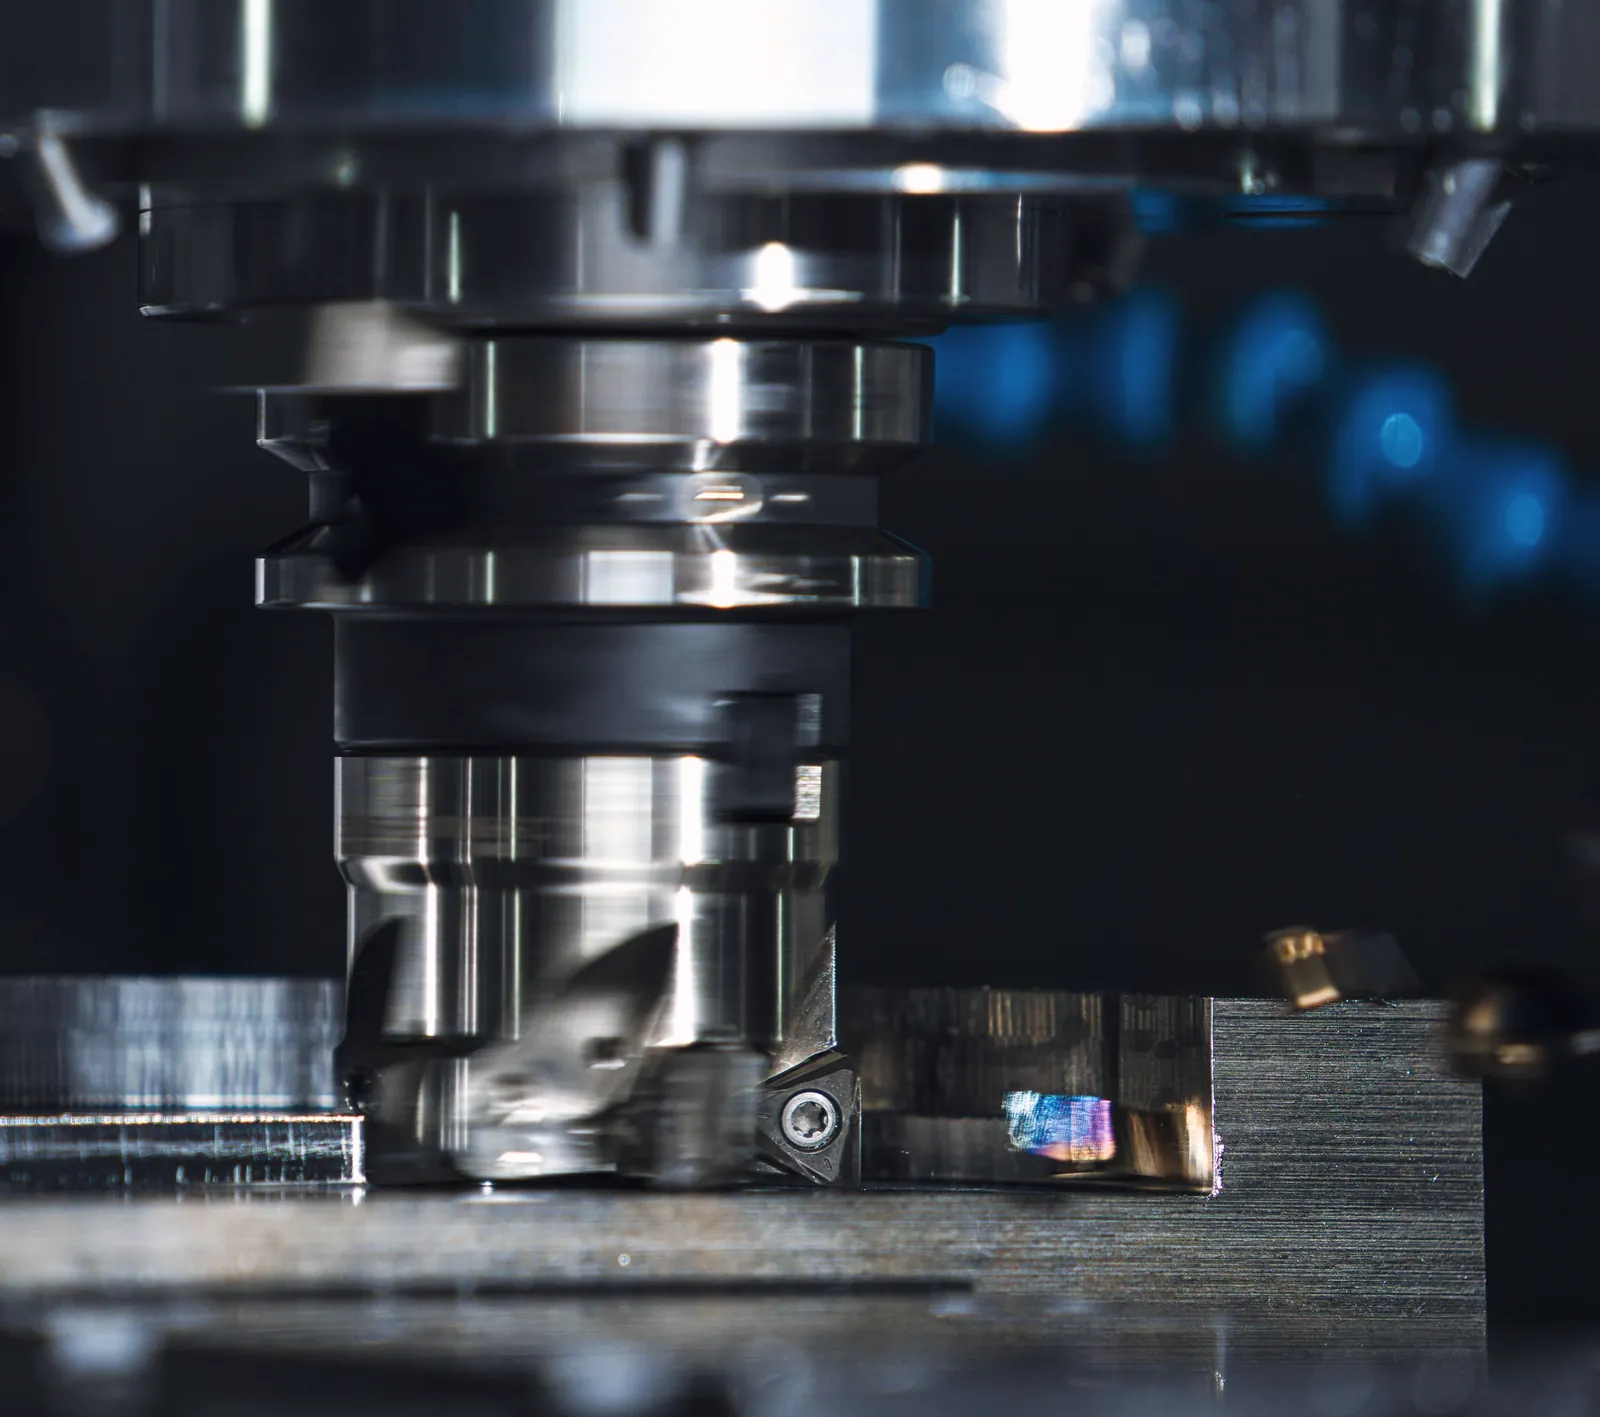
A face mill with indexable inserts cutting across the top of a steel block
Fig. 5.1Face milling a steel block
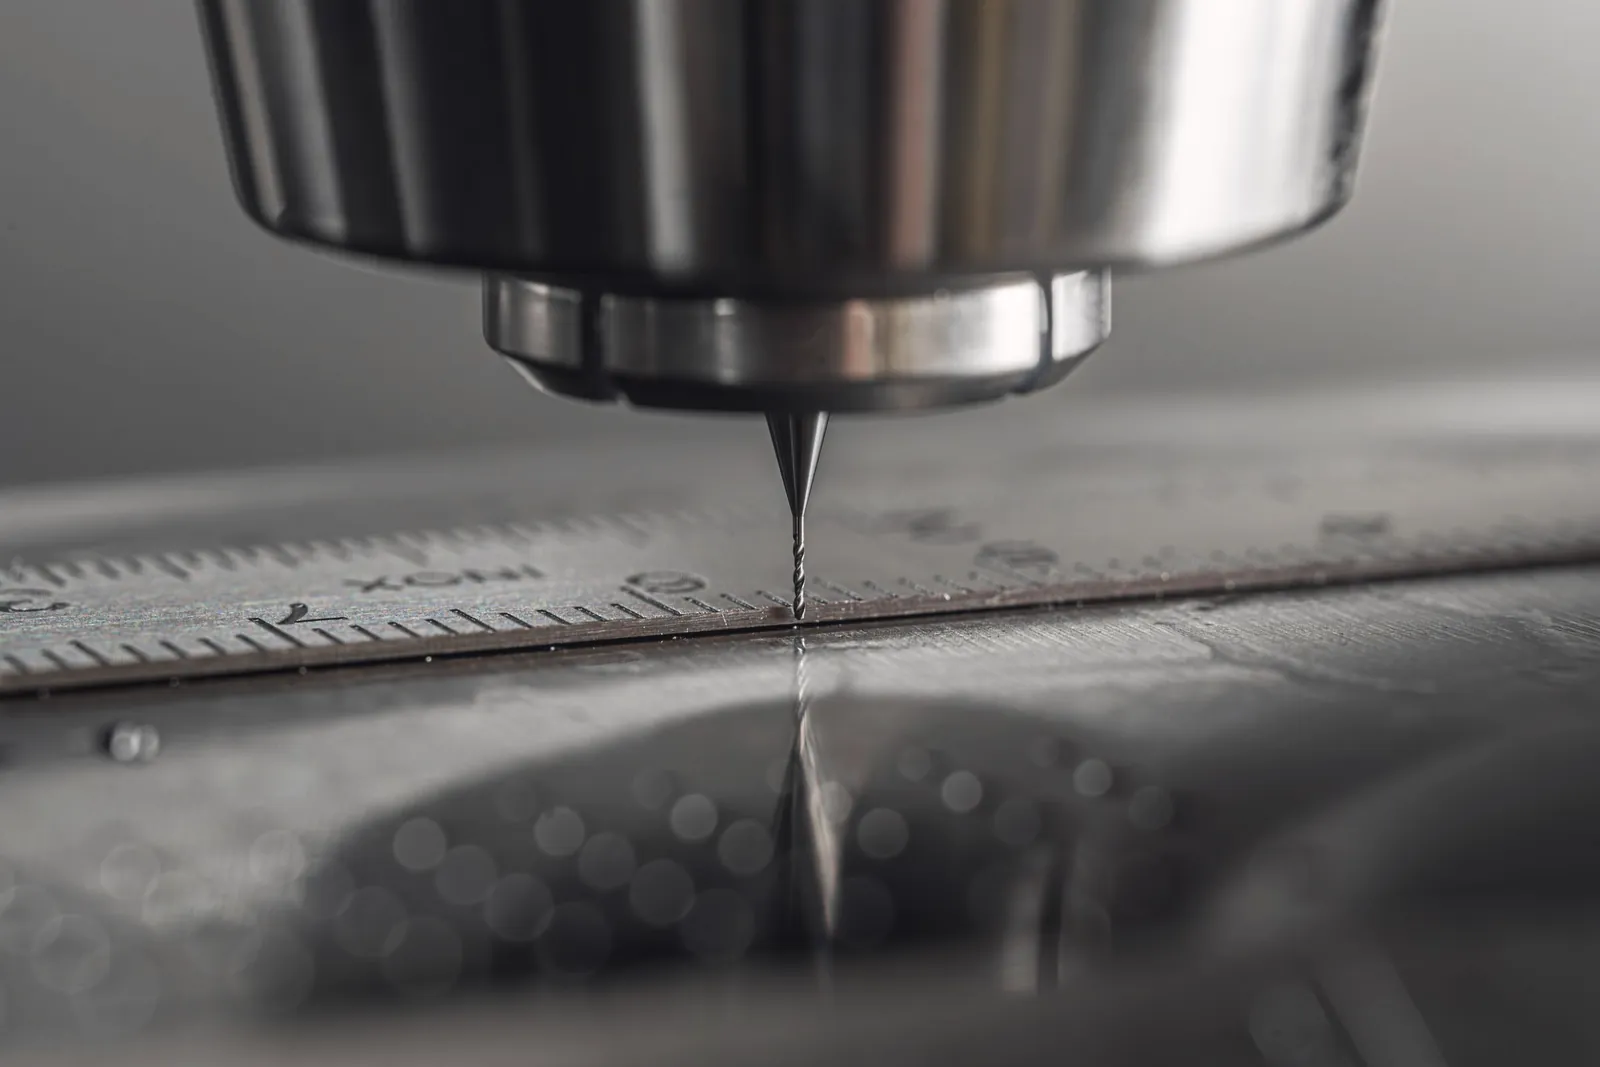
The fine point of an engraving tool just touching a metal plate
Fig. 5.2Engraving tool at the surface
MaterialProcessBatchKey tolerance
7075-T6 aluminium5-axis milling, anodise5 prototypes, then 500 a monthBearing bores H7

Request a quote

Got a drawing? Send it over.

STEP, DXF or PDF, any quantity. An engineer reads every one, and you'll have a quote within three working days.

  • STEP
  • DXF
  • PDF
  • IGES
  • Parasolid